Explore our primary collection of high-barrier, mono-material, and post-consumer recycled (PCR) packaging structures engineered for cosmetics, personal care, and specialized industries.




Leading the evolution of green cosmetic packaging and sustainable material sciences from China to the global stage.
Shanghai Boxo Beauty Co., Ltd. is a leading China Cosmetic Packaging Manufacturer, specializing in innovative and high-quality packaging solutions for the global beauty and personal care industry. With extensive experience in cosmetic packaging design, development, and production, the company provides comprehensive packaging solutions for skincare, makeup, fragrance, and personal care brands worldwide.
Our product portfolio includes cosmetic bottles, jars, tubes, airless packaging, droppers, roll-on containers, compact cases, pump dispensers, and customized packaging systems designed to meet the evolving needs of modern beauty brands. We offer a wide range of materials, including glass, PET, PP, acrylic, aluminum, and eco-friendly alternatives, ensuring flexibility for different product categories and brand positioning strategies.
Sustainability is an important part of our business philosophy. We continuously invest in environmentally responsible packaging solutions, including recyclable materials, refillable packaging systems, and lightweight designs that help brands reduce their environmental footprint while maintaining premium product appeal.
Understanding international regulatory pressures, consumer demand shifts, and the industrial transition to circular economics.
With the implementation of the European Union's Packaging and Packaging Waste Regulation (PPWR) and extended producer responsibility (EPR) programs in North America, brands face mandatory targets for recycled content. By 2030, cosmetics and consumer goods must utilize design-for-recycling principles, steering clear of complex, multi-material plastics that end up in landfills.
Modern material science is transitioning from multi-layer laminate barriers to mono-material solutions (such as 100% PP or PE tubes and bottles). These structures ensure that the physical packaging can be collected, sorted, and re-processed within existing mechanical recycling streams without contaminating the output resins.
Global beauty conglomerates are tracking Scope 3 emissions meticulously. Incorporating high-purity Post-Consumer Recycled (PCR) polymers and infinitely recyclable aluminum significantly drives down life-cycle assessment (LCA) scores, directly boosting brand equity among eco-conscious consumer segments.
How our recyclable materials adapt to specific market requirements, climates, and regional supply chain configurations.
High-end cosmetic brands in the US and Canada demand heavy-wall PCR-PET and luxury glass containers. Our custom glass bottles with serum pumps feature detachable elements, facilitating simple consumer sorting and alignment with local municipal recycling operations.
Compliance with strict EU directives dictates the use of mono-material packaging. Our 100% PP airless lotion bottles ensure that the pump mechanism, spring, chamber, and bottle body are processed as a single material stream, avoiding the costly separation steps of traditional pumps.
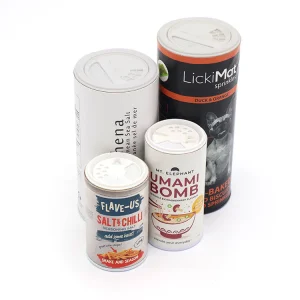
The APAC region requires lightweight, high-durability packaging capable of surviving complex logistics paths. Our kraft cylinder packaging and molded pulp designs offer superior structural cushioning for electronics and luxury cosmetics, avoiding plastic shipping fillers.
Our engineering timeline for implementing next-generation biomaterials, molecular recycling, and intelligent sorting systems.
Optimizing mechanical recycling sorting loops to deliver PCR-PP and PCR-PET with optical clarity and odor profile comparable to virgin resins. Perfecting the stabilization of PCR content up to 100% concentration without stress cracking.
Integrating non-food crop bio-based plastics (like PLA, PHA, and bio-PE) into manufacturing lines. Developing high-barrier compostable films that preserve product shelf-life while degrading safely in industrial composting environments.
Embedding invisible digital watermarks and QR tracing systems directly into mold cavities. This allows automated sorting facilities to read chemical footprints instantly and route materials to their high-value closed-loop streams.
Leveraging China's integrated industrial ecosystems to deliver cost-effective, scalable, and premium-quality sustainable packaging.
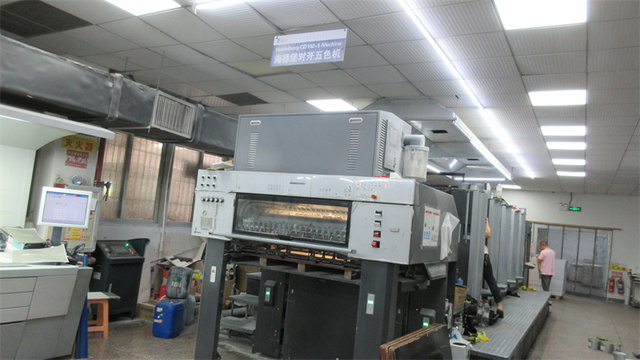
Our manufacturing headquarters in Shanghai exploits the structural advantages of China's highly integrated supply chains. Unlike fragmented manufacturing footprints, our facilities integrate material synthesis, precision injection molding, multi-layer blow molding, automatic offset printing, and final assembly under a single operational umbrella.
This vertical integration ensures that we can mitigate global raw material volatility and guarantee consistent delivery schedules. Our custom tooling shop can design, prototype, and produce high-cavitation molds in a fraction of the time required by Western toolmakers. Through advanced automated inspection technologies, we ensure that every batch of recyclable packaging meets the rigorous cosmetic tolerances of global beauty brands.
Direct partnerships with domestic chemical giants and GRS-certified collection networks ensure a stable, year-round supply of certified PCR-PP, PCR-PET, and premium aluminum alloys.
Our in-house engineering team utilizes advanced FEA modeling to optimize walls, reducing material usage by up to 20% while maintaining top-load integrity.
We are progressively transitioning our manufacturing lines to solar energy inputs and utilizing closed-loop water cooling systems to shrink our baseline factory emissions footprint.
Our packaging complies with international consumer safety laws, environmental declarations, and commercial import regulations.
Our raw materials, including PCR grades and post-consumer aluminum, comply with FDA food-contact standards, ensuring complete chemical safety for skincare formulation packaging.
Every coating, varnish, ink, and stabilizer we use is fully tested and certified free of hazardous SVHC chemicals, complying with European chemical safety regulations.
Our entire supply chain, from sourcing raw flakes to the finished bottle extrusion, is audited and certified by the Global Recycled Standard (GRS) for transparency.
We provide full Life Cycle Assessments for our core mono-material and aluminum lines, giving brands the certified carbon-offset calculations needed for sustainability reports.
A look inside our Shanghai manufacturing lines, illustrating cleanroom assembly, automated injection molding, and finished goods testing.
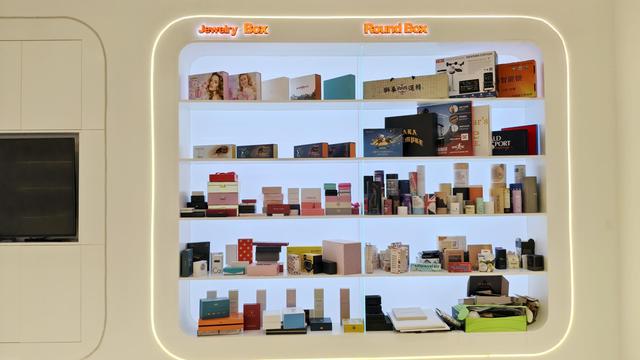
Automated Injection Molding Operations
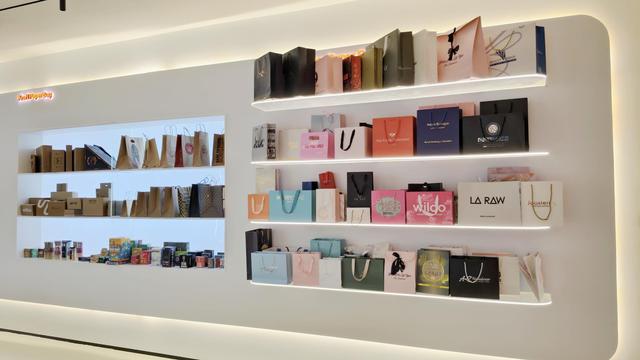
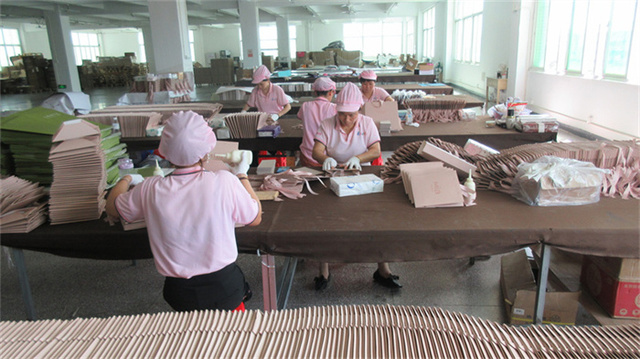
High-Speed Precision Assembly Systems
Material Purity & Integrity Inspection
Multi-Layer Cosmetic Bottle Extrusion
Eco-friendly PE Tube Header Forming
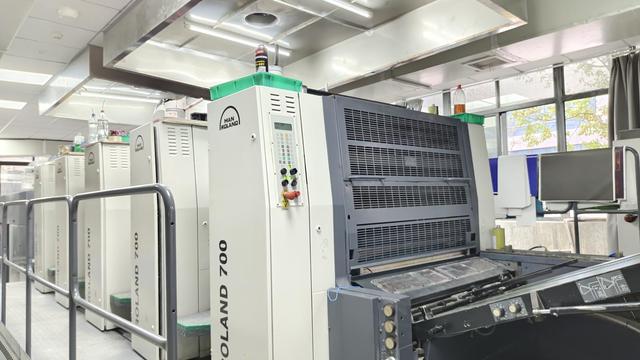
High-Precision UV Offset Printing
Finished Stock Quality Control Auditing
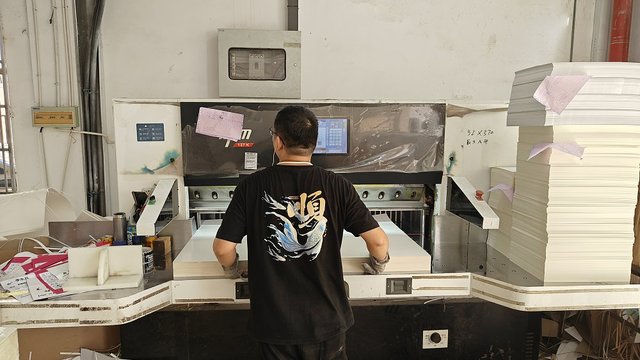
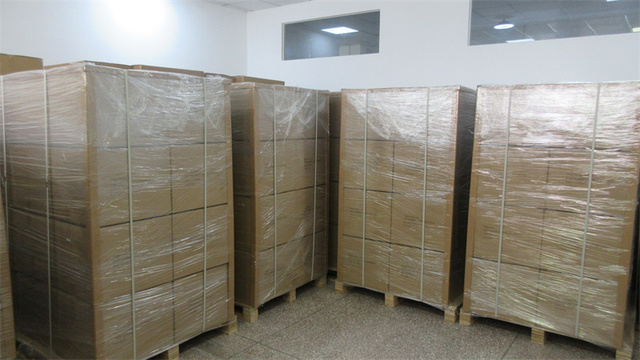
Dust-Free Packaging and Export Crating
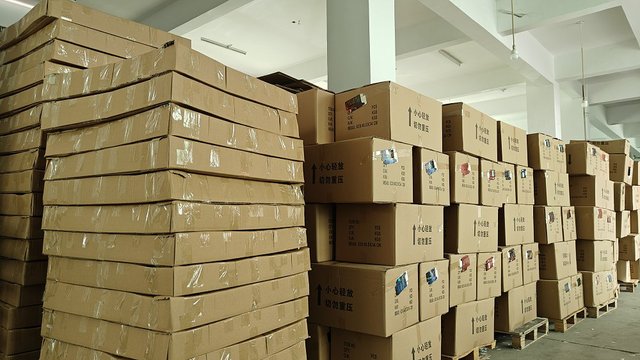
Integrated Shipping & Logistics Hub for Global Dispatch
Get definitive answers on PCR compatibility, minimum order quantities, compliance protocols, and lead times.
A: A mono-material pack is constructed from a single polymer family (such as 100% PP or 100% PE). Standard cosmetic packaging often combines multiple resins and metal parts, making sorting impossible. Mono-materials are easily sorted and processed in standard recycling streams, reducing municipal sorting costs.
A: We operate under the Global Recycled Standard (GRS) custody model. This means that every step, from raw material procurement to final extrusion, is certified by third-party auditors. We provide complete batch certifications and raw material transaction certificates (TCs) for every production run.
A: Yes. Our PCR resins undergo rigorous decontamination and molecular filtration to remove trace organic compounds and odors. We utilize food-grade PCR resins that comply with US FDA and EU EFSA requirements, ensuring they are safe for skincare and baby care products.
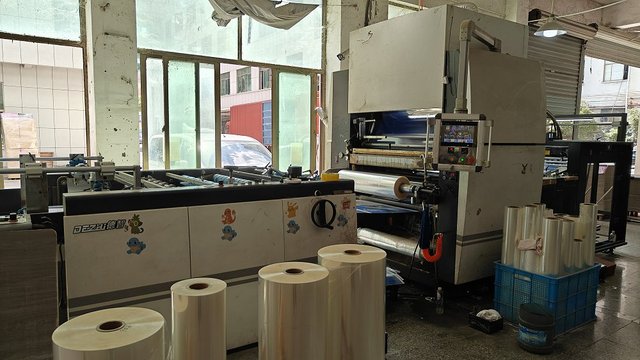
A: Yes. We offer offset printing, silk-screen printing, and water-based varnishing directly on recyclable aluminum and plastic. We use eco-friendly, soy-based, and low-VOC UV inks that do not interfere with mechanical sorting or contaminate recycled plastic batches.
A: Our MOQs vary from 5,000 to 10,000 units depending on the complexity of the material and tooling. Standard production cycles run between 25 and 35 days, which includes our multi-stage quality control checks and export packing protocols.
A: Our refillable packaging lines, such as airless bottles and jars, undergo intensive friction, cycle, and drop testing. Thread configurations and inner cup mechanisms are engineered to withstand at least 100 refill cycles without compromising the vacuum seal or pump performance.
Our secondary catalog featuring airless dispensers, high-clarity glass, and compostable storage bag designs.


 Boxo Beauty